
Formwork Fastener Delivery Inspection: A Procurement Acceptance Checklist
> In brief > - The acceptance window is narrow and unforgiving. > - Three sources must agree: the order, the packing list and the certificate. > - Record the acceptance so it survives an audit.
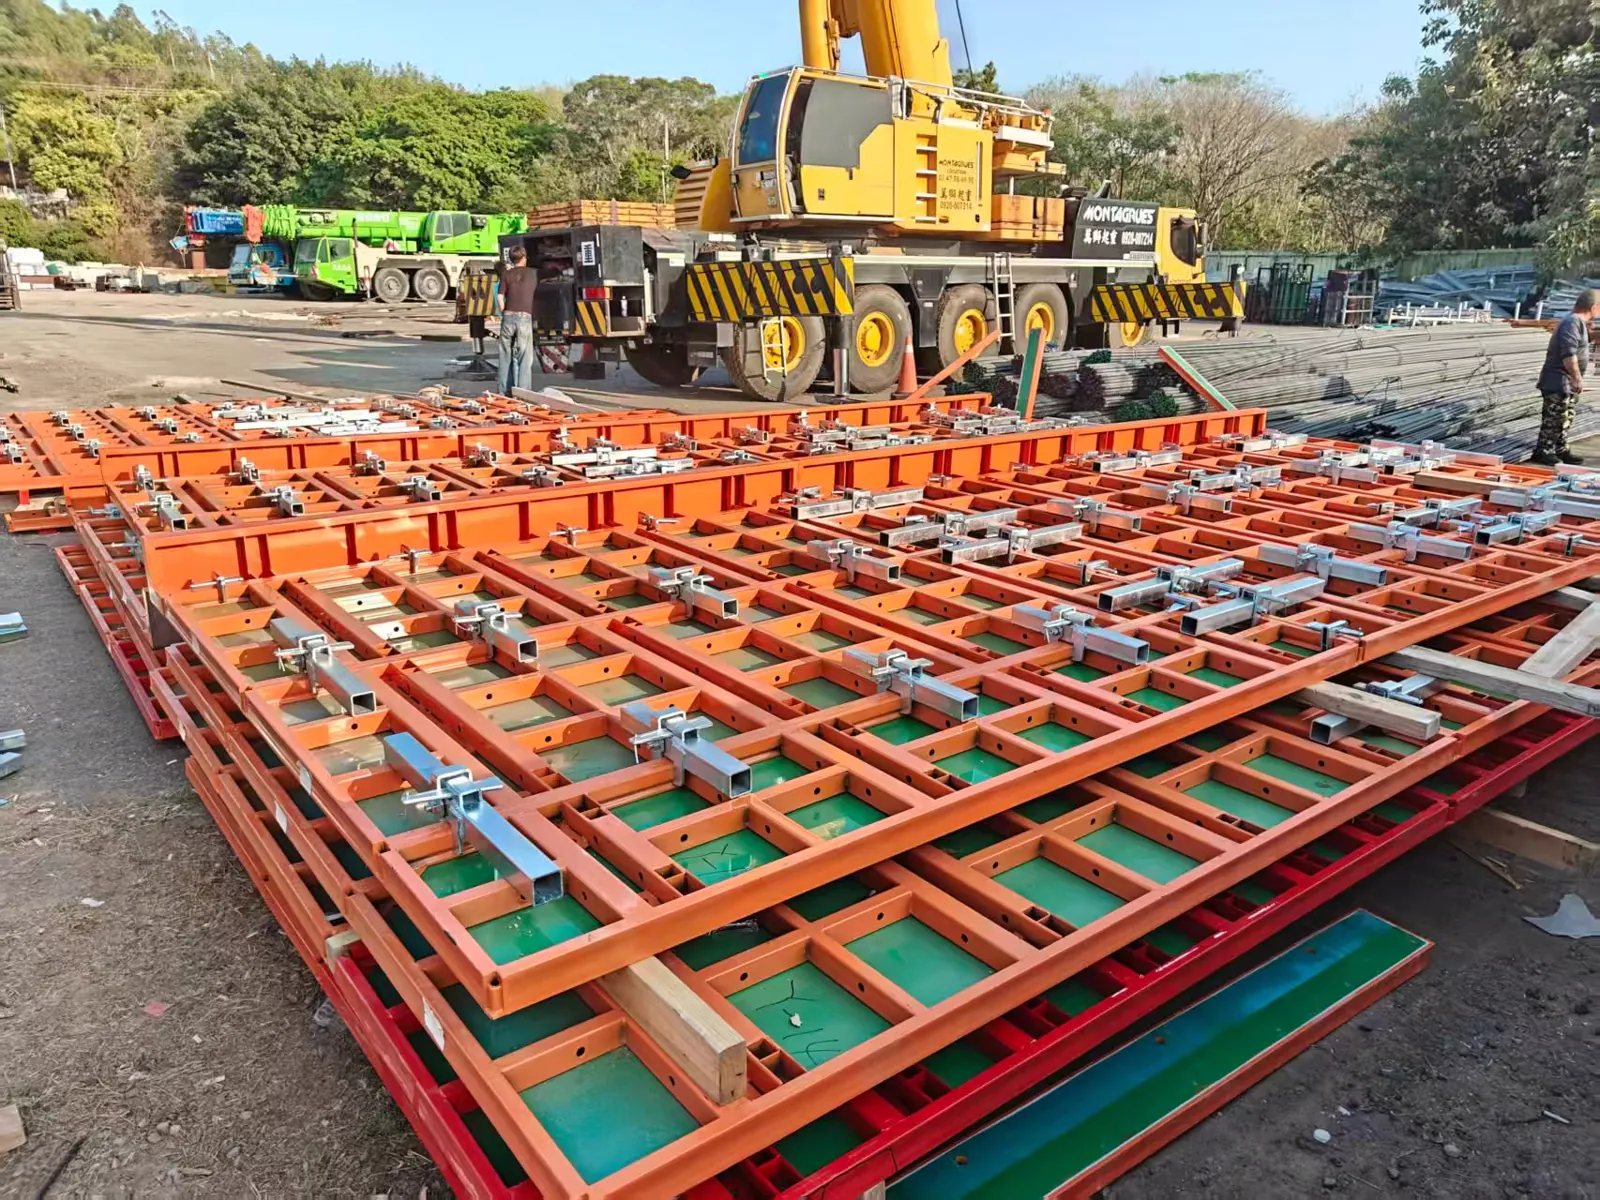
At a glance: fastener acceptance is decided at the container door, during a window of a few hours, against a purchase order that was closed months earlier. The inspection therefore has to be prepared before the goods arrive, because the commercial pressure at that moment favours unloading quickly and the technical evidence has to be gathered while the container is still sealed. Three verification streams run in parallel: documents, count, and condition. Documents establish what was contracted; count establishes how much arrived; condition establishes whether the shipment can be used. A consignment that fails any one of the three is not accepted, and the disposition differs sharply depending on which stream failed.
Ordering formwork hardware means accepting goods you did not manufacture, produced to a specification you wrote, packed by someone else's warehouse staff, and carried for weeks through ports and truck decks. The failure modes are not dramatic. They are a grade printed on a certificate that disagrees with the grade stamped on the rod, a bundle count that does not reconcile with the declared weight, a thread abraded by an inadequate separator inside the container, or a coating scratched by a forklift tine during loading. Each of these is cheap to detect at the door and expensive to detect after the first pour, when the shortfall surfaces as a wall that cannot be tied. This procedure covers what the receiving team does on arrival; the separate discipline of pre-shipment verification by a third-party inspector is covered in our article on third-party inspection scope and timing. The hazard context for handling heavy bundles on site sits within OSHA's concrete construction eTool, and the conformity framework behind the specification sits in the EU construction-products framework.
Document cross-check refers to the process of verifying that the purchase order, packing list, and mill certificate agree with each other and the contracted specifications. Count verification by weight means using the total declared weight and the average piece weight to confirm the number of pieces in the consignment. Condition inspection is the examination of a sample for thread, coating, and dimensional conformity. EN 10204 is the international standard defining types of inspection documents for steel products, with type 3.1 being the most commonly specified for construction procurement.
1. The acceptance window is narrow and unforgiving.
Container demurrage is charged per day and begins when the vessel arrives, regardless of whether anyone is ready to receive it. A consignment opened, inspected and rejected on the first morning costs one day's storage. A consignment unloaded, then discovered to be short two hundred washers during the second pour, costs a second shipment, a second customs entry and the delay itself. The economics of acceptance inspection follow directly from that asymmetry, which is why the receiving procedure is written before the goods are loaded rather than improvised at the gate.
The second pressure is physical. A twenty-foot container of tie rods holds several tonnes of steel in bundles that are difficult to turn, and a full inspection with a measuring tape and a thread gauge takes longer than the unloading crew expects. Every hour spent inspecting is an hour the container sits empty. Firms that inspect properly schedule a container-handling slot and a two-person receiving team, which converts inspection from an interruption into a scheduled operation.
2. Document cross-check: three sources that must agree.
The documentary check is the highest-yield part of the inspection because it costs no time and catches the most consequential defects. Three documents must agree with each other and with the purchase order: the purchase order itself, the packing list enclosed in the consignment, and the mill certificate issued for the heat or batch from which the parts were made. EN 10204 is the international standard defining types of inspection documents for steel products, and its type 3.1 is a document verified by the works itself and delivered with the goods, which is the level construction procurement normally specifies. See EN 10204:2004 details.
| Document | Establishes | Typical discrepancy found at the gate |
|---|---|---|
| Purchase order | The contracted grade, diameter, length, coating, thread form and certification level | Revised by amendment without the supplier acknowledging the change |
| Packing list | Bundle count, piece count, weight, carton marks | Piece count agrees with weight but bundle count differs from the certificate packing plan |
| Mill certificate 3.1 | Chemical composition, mechanical properties, heat number | Grade designation uses a different national system, so Q345 appears as St52 or as an equivalent designation |
| Delivery note | Carrier consignment reference, gross and net weight | Gross weight inconsistent with the declared packing, which points to undeclared dunnage or a different packing configuration |
Grade designation is the single most common documentary problem, because a Chinese grade such as Q345 or Q235 is frequently certified under an equivalent European designation and a supplier may transmit the certificate without translating it. The receiving engineer has to confirm that the stated values satisfy the specification rather than assuming the names correspond. ISO 9001 requires that the certificate match the delivered goods, so an unexplained mismatch is a valid ground for withholding acceptance until it is closed.
Standard basis: EN 10204:2004 details
3. Count verification by weight rather than by tally.
Counting several thousand tie rods by hand is slow and inaccurate, and the tally sheet produced under time pressure is worse than useless because it documents a number nobody verified. The reconciliation method is faster and more defensible. Weigh a representative number of bundles, calculate an average piece weight from the packing list bundle counts, then compare the total declared weight against the calculated weight for the declared piece count. Agreement within roughly one percent indicates a coherent consignment; a larger divergence points to a piece-count error, a different grade being shipped, or missing dunnage.
| Verification step | Method | Acceptance indication |
|---|---|---|
| Bundle reconciliation | Compare physical bundle count against the packing list bundle count | Exact agreement on bundle count; investigate any difference before unloading |
| Average piece weight | Weigh three bundles, divide by the pieces each contains | Within one percent of the theoretical weight for the declared diameter and length |
| Gross to net comparison | Subtract declared dunnage and packing weight from gross vehicle weight | Residual equals declared net weight within measurement tolerance |
| Length spot check | Measure the full length of ten random pieces plus the two exposed ends | Within the specified length tolerance, which is covered in our tolerance specification |
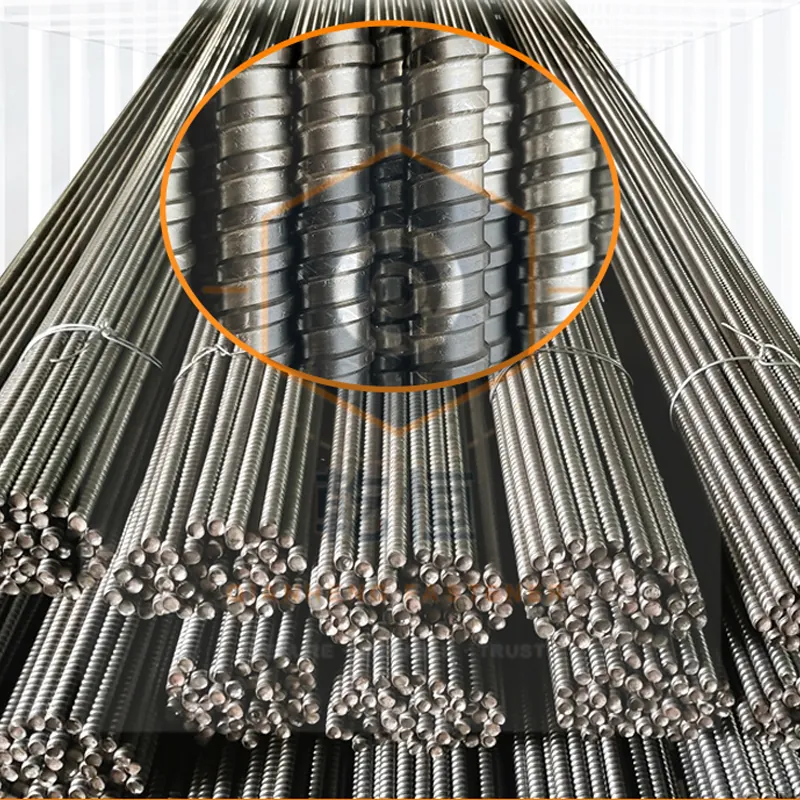
The two ends deserve particular attention, because a tie rod that is correct overall can still be unusable. The end threads may be buried in the bundle by an incorrect packing arrangement, bent by a fork lift tine, or deformed so that a nut will not start. Rod end condition is visible without disassembly and it governs whether the shipment can be used at all. We grade our tie rods to Q235, Q345, 45# and QT450 on request, and the grade can only be verified at the gate if the receiving team knows which grade it ordered.
4. Condition inspection: thread, coating and dimensional conformity.
Condition inspection is performed on a sample drawn according to a stated plan rather than on every piece. Every-piece inspection of an export consignment is neither economically possible nor necessary, since manufacturing variation is not random across a batch but clustered within heats and production runs. The receiving team should record which plan it applied, because an undocumented inspection is difficult to defend later.
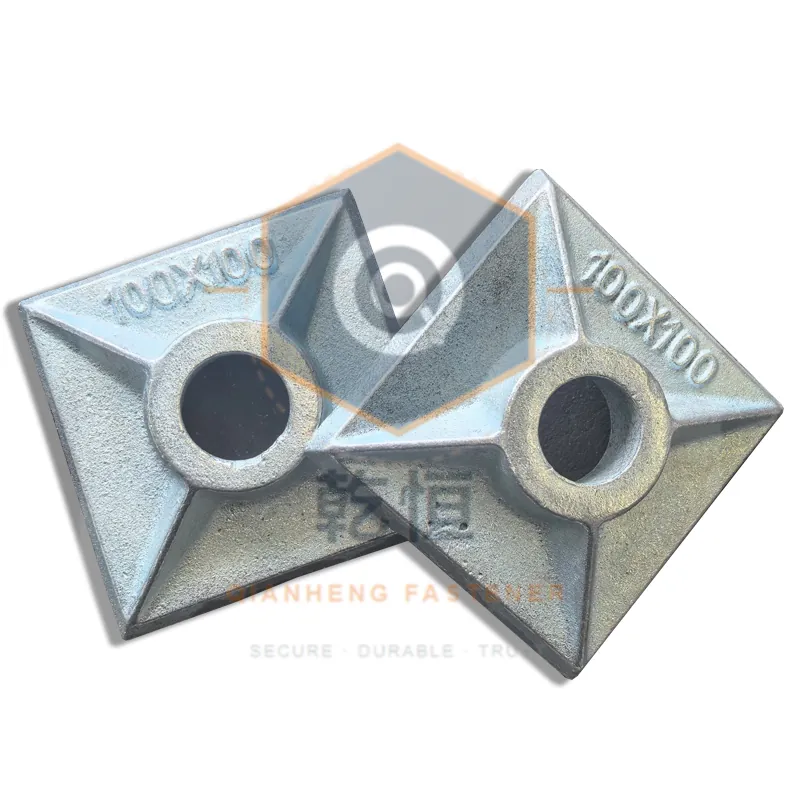
Thread condition is the most consequential physical check on any of the components shown in our D15 and D20 tie rod range. A thread that has been abraded, rusted or deformed may not accept a nut without cross-threading, and a nut that cross-threads on the first turn damages the rod in service. The inspection consists of running a nut the full length of the thread on sampled pieces and observing whether it rotates smoothly, whether the flanks show scoring, and whether any rust is present in the root of the thread. Thread form and fit across the systems we supply are covered in our reference on thread standards and forms. Coating condition is assessed by looking for abrasion, particularly on the underside of bundles where loading equipment bears, and for white rust on hot-dip galvanized surfaces, which indicates wet storage rather than handling damage. The coating systems this inspection refers to are compared in our guide to coating selection for fasteners.
| Checked item | Test applied | Rejection basis |
|---|---|---|
| Thread form and fit | Nut run full length on sampled pieces | Any piece that will not start or that cross-threads |
| Thread corrosion | Visual and root inspection under magnification | Rust in the thread root, or any evidence of stored wet |
| Coating continuity | Visual for abrasion and white rust; thickness verified where coating class was specified | Coating loss sufficient to reach the substrate over a measurable area |
| Dimensional conformity | Length, thread length and diameter on sampled pieces | Out of tolerance beyond the agreed measurement allowance |
| Physical damage | Straightness, dents, bundle strap damage | Bent rod or a flattened section preventing nut travel |
Acceptance number is the point at which a sampled batch fails the plan, and it is the figure that determines whether a shipment passes or fails. Sampling follows a recognised standard rather than an improvised rule, and ISO 2859-1 defines the plans, sample sizes and acceptance numbers that make a sampling decision defensible. The important discipline is stating the plan in advance and applying it identically, because a sampling result is only comparable if the method is identical. Where coating thickness forms part of the contracted specification, a coating thickness reading on a handheld gauge takes under a minute per point and is worth performing on at least three pieces per bundle sampled.
Standard basis: ISO 2859-1 — Sampling procedures for inspection by attributes
5. The disposition decision: reject, partial accept, or accept with concession.
Every inspection ends in one of three dispositions, and choosing between them is a commercial judgement supported by technical evidence rather than a purely technical outcome. The evidence gathered in the previous sections determines which disposition is proportionate.
Three preparation steps materially shorten the inspection window:
- Agree the sampling plan and the disposition template with the supplier before the order is placed
- Appoint a two-person receiving team and book a container-handling slot at the destination
- Issue the document list the receiving team will check against, including the required certificate type
Rejection applies where the failure cannot be worked around. A wrong grade, a documentation mismatch that cannot be closed, or thread damage affecting a significant share of the sampled pieces means the consignment does not correspond to the purchase order and cannot be put into service. Rejection at the door preserves the option of replacement, which remains available because the goods are still at the port.
Partial acceptance applies where the failure is confined to identifiable lots within an otherwise conforming consignment, which is the common case for coating damage localized to the bottom of a stack or count errors confined to one bundle. Segregate the accepted portion physically, photograph and weigh the rejected portion, and record both against the packing list marks. Freight and duty then settle on the accepted quantity, and the rejected portion is either returned or disposed of according to the contract terms.
Acceptance with concession applies where the deviation is cosmetic or irrelevant to function. Coating abrasion over a small surface area, a minor dimensional deviation inside the measurement allowance, or a documentation formatting irregularity that the supplier closes in writing typically qualify. Concessions should be recorded in writing by both parties at the point of acceptance, because a concession granted verbally at the gate becomes a dispute when the invoice is settled.
6. Recording the acceptance so it survives an audit.
The inspection record is the deliverable of this entire procedure. Every procedure at our works is reviewed by a second engineer before issue, and the same discipline is applied to the templates a receiving team works from. Company background, certification scope and production capacity are set out on our about page, and the inspection procedure described here is written against that documented capability. The record should identify the consignment, the purchase order and its amendments, the documents received and those outstanding, the sampling plan applied with its sample size, every nonconformity found with photographs, the disposition granted, and the names of both signatories. Keep photographs of the pallets as received, the bundle marks, and each defect, since images taken before unloading are the only unbiased record of how the consignment arrived.
The receiving checklist is also the first document a supplier works from after the contract is awarded, so it is worth issuing a matching brief with the order. Our article on how to write a fastener RFQ covers the specification side of that same transaction. Where the receiving team wants a template or a supplier-side confirmation before the vessel arrives, send the consignment details to our engineering team and the document set is returned with the checklist attached. Records are also the basis of any subsequent claim. Where the supplier accepts a concession, the written concession document references the inspection record, which prevents a later dispute about whether the deviation was known at the time of unloading. Where the consignment is rejected, the record supports both the replacement claim and any application for demurrage relief, since it evidences the exact hour at which the goods were opened and found non-conforming.
Storage after acceptance deserves one closing instruction. Steel fasteners accepted into an open yard begin accumulating corrosion risk from the moment of unloading, particularly where hot-dip galvanized surfaces face standing water. Bundles should be stacked off the ground, tilted to shed water, and segregated from stainless steel, since carbon steel particles in contact with stainless surfaces cause pitting that appears weeks later. This matters most for the components intended for reuse, because a recoverable tie rod pitted at the thread root has already lost part of its service life. Our article on running tie rods as site assets covers the accounting side of that decision.
References and standards.
- ISO 2859-1 — Sampling procedures for inspection by attributes
- ISO 9001:2015 — Quality management systems
- EN 10204:2004 — Types of inspection documents
- NIST material measurement standards
- EN 13670 — Execution of concrete structures
- ACI 347 — Guide to formwork for concrete
About us: This article covers formwork fastener delivery inspection and the acceptance checklist. Our team specializes in manufacturing high-quality formwork fasteners. Our contact page provides a way to reach our support team, and the about page documents our company's history and capabilities. This article was reviewed by the Qianheng Formwork Engineering team.