
Coating Choice: Black Oxide, Zinc, Hot-Dip and Dacromet
> In brief > - "Galvanised" is not a specification — thickness and method are. > - Hot-dip galvanising to ISO 1461 means at least 45 microns; electro-plating commonly means 5 to 12. > - Coating thickness is what decides the life of the part, not the name on the invoice.
Coatings are chosen on three axes: how long the part must last, whether the thread must still assemble, and whether the steel grade is sensitive to hydrogen. Optimizing one axis at the expense of the others is the usual cause of coating complaints.
Our own production and test data are available on request — see how our factory works and contact the engineering team for the documents behind any figure quoted here.
Coating thickness refers to the physical depth of the protective layer applied to the fastener, which directly affects its durability and performance. Salt-spray life means the duration a coated fastener can withstand exposure to a salt spray test, indicating its corrosion resistance. Thread fit is the compatibility between the male and female threads after coating, critical for ensuring proper assembly. Hydrogen embrittlement refers to the process where high-strength steel absorbs hydrogen during plating, leading to potential delayed cracking if not properly baked.
The four common finishes.
BLACK OXIDE: a conversion coating 1-2 µm thick. Decorative, mildly oil-retentive, salt-spray life measured in hours. Use it indoors, for dry storage, and where dimensional change must be zero.
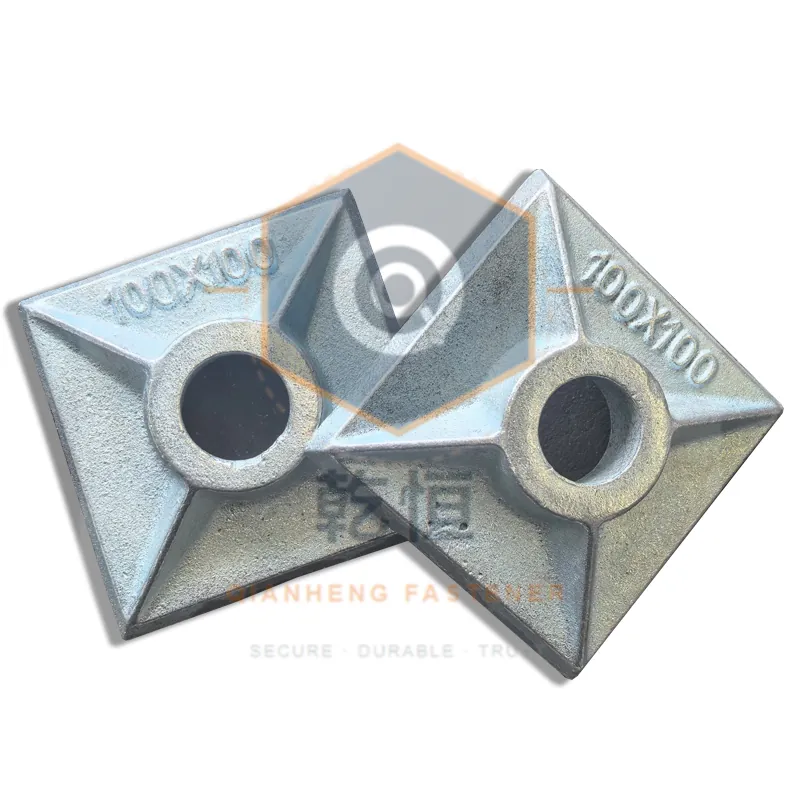
ELECTRO-GALVANIZING: 5-25 µm of zinc, uniformly applied and thread-friendly because thickness is predictable. Salt-spray life roughly 100-300 hours depending on thickness and passivation. The default for sheltered outdoor use and for parts that must assemble freely.
HOT-DIP GALVANIZING (HDG): 45-85 µm, metallurgically bonded, salt-spray life above 1000 hours in rural and urban atmospheres. The correct choice for permanent embedment — anchors, base plates, prestressed bars left in the structure — and for coastal sites. The cost is dimensional: coating builds on threads and requires tapped-oversize nuts or re-tapping after coating.
ZINC-LAMELLAR (e.g. Dacromet type): 8-12 µm of zinc-aluminium flakes in a binder. Salt-spray life around 500-1000 hours, no hydrogen embrittlement because the process is not electrolytic, and no thread blocking. The standard answer for class 10.9 and above where HDG is impractical.
Standard basis: ISO 1461
The hydrogen embrittlement trap.
Any acid-cleaned, electroplated high-strength part absorbs hydrogen. Class 10.9 and above must be baked within a defined window after plating — typically within four hours, at 190-220 °C for four hours or more, depending on the standard — and the processor must record it. Without the bake, delayed cracking can appear at 24-72 hours. If you buy electroplated 10.9 fasteners, require the baking record. If the processor cannot produce it, change the finish.
Standard basis: ISO 10683:2018 — Fasteners — Zinc flake coating systems
Thread fit arithmetic.
A 60° metric thread has two flanks, so coating on both flanks consumes pitch diameter at roughly four times the coating thickness. A 60 µm HDG coating therefore reduces effective clearance by about 240 µm on pitch diameter — enough to make a 6g/6H assembly impossible. The usual fixes: tap nuts oversize after coating, allow a coating-specific clearance in the class, or specify a coating that does not build.
Selection rules.
Indoor, dry, frequently reused: black oxide or thin electro-galvanizing; nothing that blocks threads.
Sheltered outdoor, temporary works, frequent assembly: electro-galvanizing 12-25 µm.
Permanent embedment, coastal or high-humidity site, long design life: hot-dip galvanizing 45-85 µm with matched oversize nuts.
High-strength steel (10.9+) where coating is required: zinc-lamellar or mechanical plating; avoid electroplating.
Mixed assemblies: one coating system per joint. A galvanized rod with a bare steel nut creates a galvanic couple; the nut corrodes preferentially and the joint loosens.
Specification language that prevents disputes.
Write the finish as a standard plus a measured range, not as a word. "Galvanized to ISO 1461, minimum local thickness 45 µm, average 55 µm" is auditable. "Galvanized" is not, and it is the phrase most often at the centre of a rejected shipment.
| Coating Type | Salt-Spray Life (hours) | Consequence for Design and Use |
|---|---|---|
| Black Oxide | Hours | Use indoors, dry storage, no thread block |
| Electro-Galvanizing | 100-300 | Sheltered outdoor, frequent assembly, thread-friendly |
| Hot-Dip Galvanizing | >1000 | Coastal sites, permanent embedment, requires oversize nuts |
| Zinc-Lamellar | 500-1000 | High-strength steel, no hydrogen embrittlement, no thread block |
References and standards.
- ISO 1461:2022 — Hot dip galvanized coatings on fabricated iron and steel articles
- ISO 10683:2018 — Fasteners — Non-electrolytically applied zinc flake coating systems
- ASTM A36/A36M — Standard specification for carbon structural steel
- ASTM A615 — Standard specification for deformed and plain carbon-steel bars
- NIST corrosion and materials data
- EN 10204:2004 — Types of inspection documents
- ISO 898-1 — Mechanical properties of fasteners made of carbon steel
About us: This article compares coating options for formwork fasteners, checked against our production and test data. Our factory is equipped to apply and test all the coatings discussed. Our contact page provides access to the engineering team for detailed inquiries, and the about page documents our manufacturing capabilities. This article was reviewed by the Qianheng Formwork Engineering team.